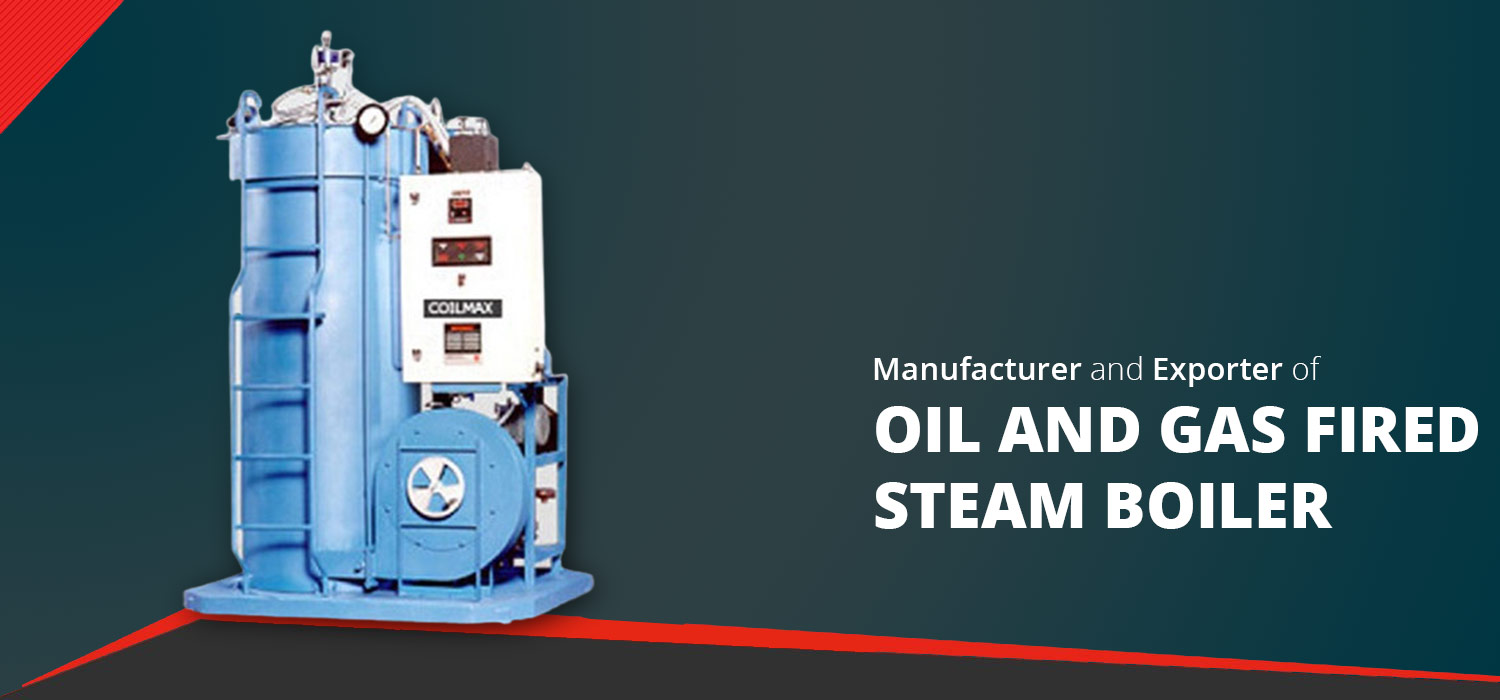
500-1000 kg-hr IBR Approved Water Tube Boiler About
500-1000 Kg HR IBR Approved Water Tube Boiler is an industrial boiler that uses water tubes to circulate the hot gases created by fuel combustion. The boiler must adhere to these rules and meet the safety and quality standards established by the Indian government in order to receive IBR certification. 500-1000 Kg HR IBR Approved Water Tube Boiler contains water inside tubes while hot gases circulate around them. Because of the increased surface area for heat exchange, the process is more efficient and produces steam more quickly. Power plants, chemical plants, and other industrial settings that call for high-pressure steam frequently employ this boiler.
Versatile Multi-Fuel PerformanceWith its ability to utilize a range of fuels such as coal and biomass, this IBR-approved water tube boiler is adaptable to diverse operational needs. The multi-fuel capability allows industries to optimize fuel consumption based on availability and cost, making it an economical and sustainable choice for steam generation.
High Efficiency Steam GenerationEngineered with precision, the boiler ensures high-efficiency output, supplying consistent steam for a wide range of industrial processes. Its advanced water tube construction maximizes heat transfer while maintaining safety, and its robust steel material guarantees durability and minimal maintenance.
Reliable Indian ManufacturingProduced and exported from India, this water tube boiler meets stringent IBR standards, offering quality assurance to manufacturers and suppliers worldwide. Its design supports high-temperature operation and long service life, addressing the critical demands of industrial steam production.
FAQ's of 500-1000 kg-hr IBR Approved Water Tube Boiler:
Q: How does the 500-1000 kg-hr IBR Approved Water Tube Boiler work?
A: This boiler operates on a water tube principle where water circulates inside the tubes and is heated externally by combustion gases generated from multi-fuel sources. The process efficiently converts water into steam, which is then used for various industrial applications.
Q: What are the key benefits of choosing this water tube boiler?
A: Its main advantages include high thermal efficiency, long operational life, compatibility with multiple fuels, reliable steam output, and adherence to IBR safety standards. This makes it a cost-effective and environmentally friendly solution for industrial steam needs.
Q: When is this water tube boiler most suitable for use?
A: The boiler is ideal for industries that require consistent, high-volume steam generation, especially in environments where fuel variability or high efficiency is a priority. It suits manufacturing, processing, chemical, and other heavy industries.
Q: Where is the 500-1000 kg-hr water tube boiler typically used?
A: It is commonly used in industrial settings across India and exported globally, serving factories, refineries, power plants, food processing units, and other sectors that rely on continuous steam generation.
Q: What is the process for installing and commissioning this industrial boiler?
A: Installation involves secure positioning, integrating multi-fuel supply lines, and connecting to the steam distribution system. Commissioning is performed by certified engineers to ensure compliance with IBR regulations and operational safety.
Q: How can operators optimize fuel consumption with this boiler?
A: By selecting the most efficient and available fuel-coal, biomass, or others-operators can manage costs and optimize performance. Regular maintenance and monitoring operational parameters also help achieve peak efficiency.


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese


 Send Inquiry


 Send Inquiry