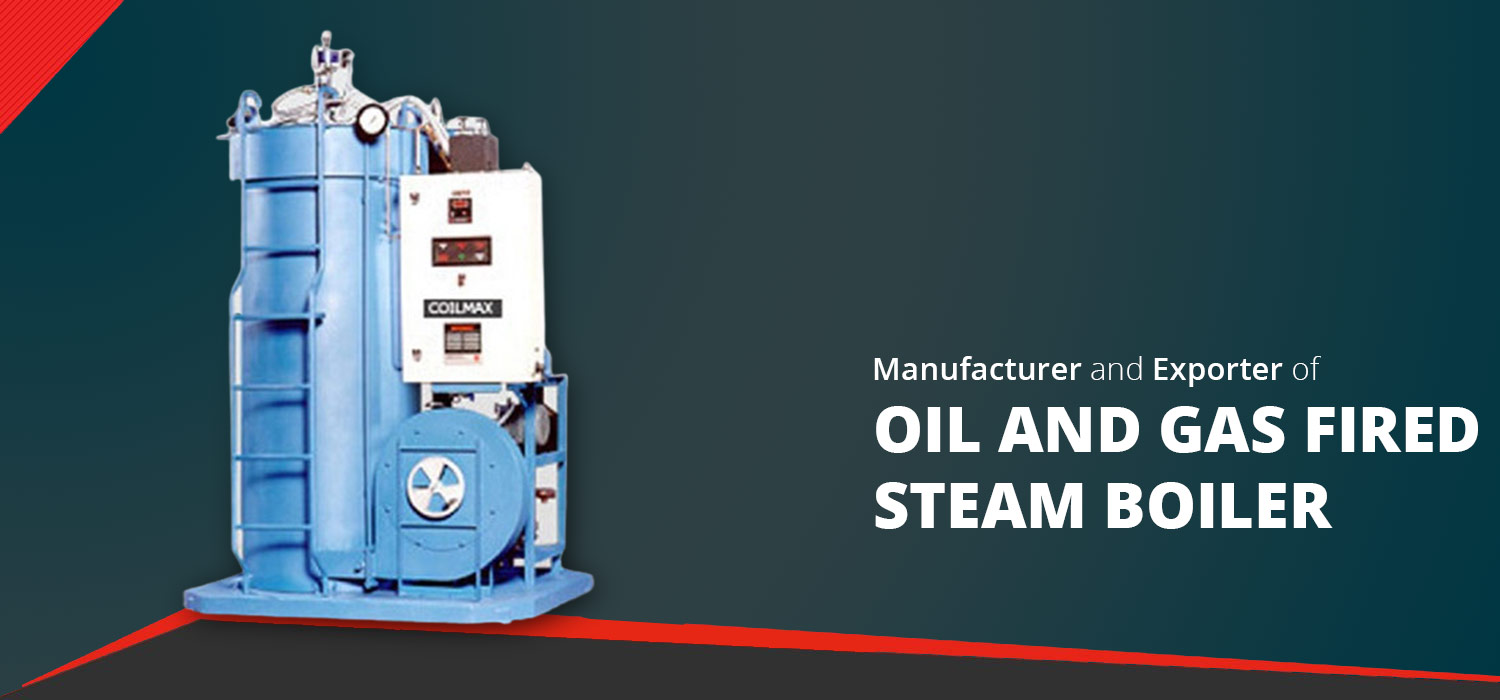
Oil Fired 1500 kg-hr IBR Approved Package Steam Boiler About
We have attained the level of excellence in making Oil Fired 1500 kg-hr IBR Approved Package Steam Boiler finds its applications in the HVAC systems for water heating, sanitation and waste energy utilization. All our items are tested on the various quality parameters before dispatching them from our premises. The formation of the described Package Steam Boiler is done by using best quality required material. We offer the same at common market price rate within the promised time frame.
Advanced Automation and SafetyThis steam boiler integrates state-of-the-art automation technology, ensuring safe and precise operation. The automatic controls regulate pressure, temperature, and steam output, reducing the need for manual intervention and eliminating potential operational errors. The shell tube design, combined with IBR approval, guarantees strict adherence to quality and safety standards, meeting the demanding requirements of industrial applications.
Efficiency and PerformanceDesigned to maximize energy savings, the boiler achieves a high heat efficiency of 882%. It delivers a consistent output of 1500 kg/hr of dry saturated steam, essential for hospital sterilization and other sensitive industrial processes. The robust construction using stainless steel enhances heat retention, translating into reduced fuel consumption and lower operational costs.
Versatile Installation and ApplicationThe skid-mounted configuration of this steam boiler streamlines the installation process, allowing for easy mobility and integration into new or existing plant setups. Its compact footprint and automatic operation make it suitable for a variety of industries-particularly in hospitals-facilitating uninterrupted steam supply and improved workflow productivity.
FAQ's of Oil Fired 1500 kg-hr IBR Approved Package Steam Boiler:
Q: How does the skid-mounted design benefit the installation process of the boiler?
A: The skid-mounted design simplifies installation by providing a pre-assembled, compact package that can be easily placed on-site, reducing setup time and minimizing disruption to other operations. This also allows seamless relocation if operational requirements change.
Q: What makes this steam boiler suitable for hospital applications?
A: Its ability to produce a reliable and steady supply of dry saturated steam at 1500 kg/hr is crucial for hospital sterilization and hygiene. The automatic controls and high heat efficiency ensure consistent performance, safety, and energy savings, aligning well with hospital demands.
Q: When should the boiler be maintained to ensure optimal performance?
A: Routine maintenance is recommended as per the manufacturer's schedule, typically including inspections and cleaning every few months, and comprehensive servicing annually. Timely maintenance helps preserve energy efficiency and prolongs the unit's lifespan.
Q: Where can this boiler be applied apart from hospitals?
A: This package steam boiler is also suitable for other industrial environments such as food processing, pharmaceuticals, textiles, and manufacturing, where dependable and high-quality steam is crucial for various operational processes.
Q: What is the process for generating steam in this shell tube type boiler?
A: Oil fuel is combusted within the boiler to heat the shell tube assembly. The heat transfer process converts water into dry saturated steam, which is then delivered at a controlled pressure of 10.54 kg/cm2 for industrial use.
Q: What are the key benefits of choosing an IBR approved package boiler?
A: IBR approval signifies compliance with strict Indian standards for safety, durability, and performance. Coupled with automatic operation and a high heat efficiency rating, this ensures peace of mind, lower fuel consumption, and reliable steam output for critical applications.


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese


 Send Inquiry


 Send Inquiry